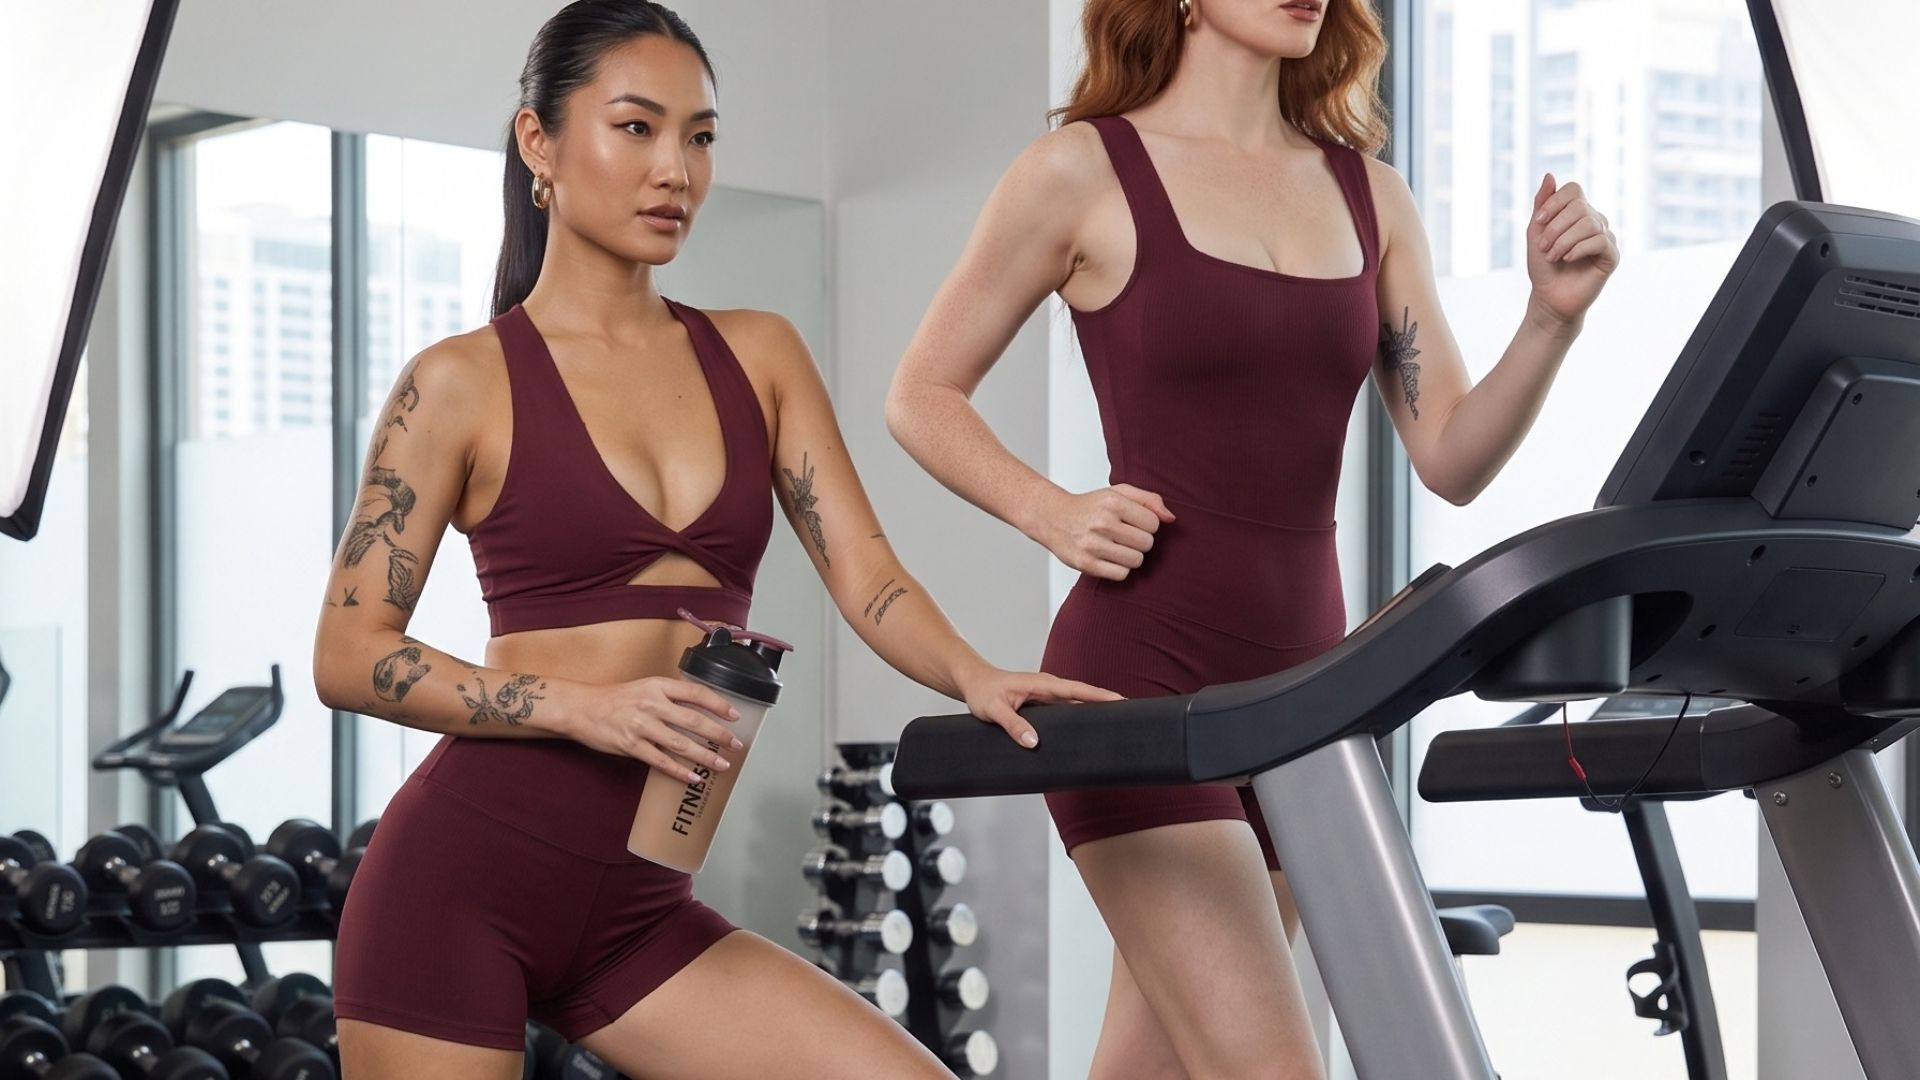
When launching, growing, or scaling a fitness apparel brand in today’s fiercely competitive athleisure and sportswear market, the long-term success, profitability, and reputation of your collection depend heavily on two foundational pillars: expert fabric selection and uncompromising manufacturing precision. Modern consumers no longer view gym wear as an afterthought; they demand high-performance apparel that seamlessly bridges the gap between intense, sweat-heavy workouts and effortless, stylish everyday athleisure.
Unlike standard casual fashion, activewear must constantly endure severe physical stress, rigorous body movement, and industrial laundering. Technical garments must perform flawlessly under intense pressure, actively manage moisture through rapid evaporation to keep athletes dry, and stretch dynamically in all directions without ever losing structural shape, support, or opacity. Furthermore, the material must feel exceptionally soft, frictionless, and comfortable against the skin to prevent chafing during prolonged use.
Whether you are designing high-compression gear for grueling CrossFit and HIIT sessions, supportive sports bras for running, or buttery-soft lifestyle pieces for daily wear, having a deep, practical understanding of technical textiles is vital for any brand founder, indie designer, or wholesale buyer. Navigating the nuances of GSM weights, fiber compositions, and yarn elasticity can make or break a product launch.
This comprehensive guide breaks down the core material categories every fitness entrepreneur needs to master. From advanced moisture-wicking synthetics and double-brushed comfort knits to specific factory-tested fabric options and strict quality assurance protocols, this overview is designed to help you navigate production with absolute confidence, elevate your product quality, and eliminate costly manufacturing mistakes from your supply chain.
1. Moisture-Wicking Synthetics
When designing activewear, one of the most critical engineering challenges is moisture management. Natural fibers such as standard cotton are inherently hydrophilic, meaning they absorb and hold onto moisture. During strenuous physical exercise, cotton traps sweat directly against the skin, leading to heavy, damp garments, uncomfortable skin chilling during cool-down periods, and painful friction or chafing. Activewear requires advanced high-performance synthetics engineered specifically to manage perspiration through capillary action (or wicking), pulling sweat away from the body and dispersing it across the exterior of the fabric where it can evaporate rapidly, ensuring athletes remain dry, light, and comfortable even during peak exertion.
- Performance Polyester & Recycled Microfibre (4-Way Stretch): Polyester is naturally hydrophobic, meaning it repels water rather than absorbing it, actively transporting sweat to the outer surface of the garment for rapid, cooling evaporation. For modern eco-conscious performance lines seeking sustainability without sacrificing technical specs, our Recycled Microfibre 4-Way Stretch (86% Recycled Polyester, 14% Spandex, 135 GSM)offers a featherlight, highly flexible solution. Its 4-way stretch capability allows the fabric to expand and contract smoothly in every direction with the body’s natural biomechanics. Available in versatile, core retail-ready shades like White, Khaki, Navy, Washed Black, and Black, it serves as an ideal material choice for ultra-breathable running shorts, lightweight training tees, and flexible outer layers that demand zero restrictions during movement.
- Nylon (Polyamide) Blends: Regarded in the textile industry for its exceptional tensile strength, superior abrasion resistance, and an unmistakably silky, luxurious hand-feel, nylon is a premier material choice for high-end activewear collections. Our Lulu line (80% Nylon, 20% Spandex, 220 GSM) provides a sophisticated matte finish, incredible long-term durability, and robust, reliable recovery for form-fitting apparel that undergoes intense friction and repeated stretching. It is offered in a curated palette of rich, premium color tones including Fog, Cognac, Oceanic, Rose, Botanical, Charcoal, Espresso, and Olive, giving luxury fitness brands and boutique athletic labels the premium visual aesthetic and heavy-duty mechanical performance their discerning clients demand.
2. Stretch, Compression, and Texture
Activewear must perform a complex mechanical balancing act: it needs to stretch dynamically with the body through extreme ranges of motion and instantly snap back to its original shape without sagging, bagging at the joints, or losing its supportive hold. Different knitting techniques, fiber blends, and fabric weights deliver varying levels of targeted compression, warmth, and tactile comfort.
- Double Brushed Performance Knits: For garments that require a buttery-soft interior against the skin without sacrificing structural compression, mechanical brushing excels. Our Juno – Double Brushed line (77% Polyester, 23% Spandex, 230–240 GSM) delivers medium-to-heavyweight compression paired with an exceptionally plush hand-feel. The mechanical brushing process raises the surface fibers of the yarn to trap a microscopic layer of warmth while maintaining breathability, making it an absolute favorite for high-performance yoga sets, leggings, and winter training pieces. It is available in a versatile color palette including White, Skin, Green, Lobster, Chocolate, Forest, Terracota, Charcoal, and Black.
- Heavy Ribbed Textures: Textured knits add structural depth, visual interest, and a fashion-forward athleisure aesthetic that transitions smoothly from the studio to the street.
- Lola Rib (63% Viscose, 34% Poly, 3% Spandex, 250–260 GSM): Features a rich 10×2 rib structure combining high breathability with a substantial, premium weight. The viscose content provides a silky drape and moisture absorption, while polyester and spandex ensure structural resilience and recovery, making it ideal for statement athleisure wear offered in shades like Charcoal, Black, Caramel, Truffle, Teal, and Rose.
- Cotton Air (100% Cotton, 210–230 GSM, 36” Tub / ~2.5M): Built from 100% pure cotton, this fabric delivers natural breathability and exceptional softness. It is perfect for pre- and post-workout layering, cozy hoodies, and lifestyle loungewear where natural comfort takes priority. It is available in a wide selection of relaxed earthy tones, including BW, Matcha, Jade Green, Lumut, Beige, Earth Brown, Brown, Rose Tan, Crockery, Metal, Star Gazer, and Jet Black.
3. Eco-Conscious Alternatives
Modern consumers increasingly demand eco-friendly apparel without compromising on athletic performance, durability, or tactile appeal. Sustainable textiles have rapidly evolved to meet strict technical standards, proving that green fashion can perform just as well as traditional virgin synthetics under rigorous athletic conditions. Sustainable activewear manufacturing is no longer just a niche market segment; it is a fundamental baseline expectation for conscious consumers who expect their workout gear to align with environmental ethics.
- Recycled Polyester (rPET) & Microfibre Blends: Utilizing post-consumer plastic bottles that are thoroughly cleaned, melted down, and spun into high-grade microfibre yarns allows modern brands to maintain elite moisture-wicking and 4-way stretch standards. For instance, integrating our Recycled Microfibre 4-Way Stretch (86% Recycled Polyester, 14% Spandex, 135 GSM) into a performance collection significantly reduces landfill waste and greenhouse gas emissions. This fabric delivers featherlight flexibility, rapid drying capabilities, and a reliable hand-feel across versatile core shades like White, Khaki, Navy, Washed Black, and Black, proving that eco-friendly materials do not require any sacrifice in athletic functionality.
- Blended Versatility & Eco-Integration: Balancing synthetic durability with sustainable fiber compositions allows modern activewear brands to cross over smoothly from high-sweat gym sessions to casual lifestyle wear. By merging recycled synthetics with eco-certified yarns, brands can achieve the ideal balance of tensile strength, shape retention, and environmental responsibility without sacrificing the technical performance required by athletes.
4. Durability & Feel
Mastering technical fabric specifications requires a thorough understanding of GSM (grams per square meter)—the industry standard metric measuring fabric density, weight, and material compactness—alongside precise yarn compositions. Fabric GSM fundamentally dictates the structural drape, thermal retention, opacity under tension, and ideal end-use application of every finished garment.
- Lightweight (135–150 GSM): Represented by our Recycled Microfibre 4-Way Stretch (86% Recycled Polyester, 14% Spandex, 135 GSM). At this featherlight weight, the fabric offers exceptional breathability, rapid heat dissipation, and unrestricted flexibility. Its primary characteristics include quick-drying ventilation and a weightless feel against the skin, making it ideal for ultra-lightweight running shorts, breezy sports tops, and flexible inner linings.
- Mediumweight (210–240 GSM): Represented by our Lulu (80% Nylon, 20% Spandex, 220 GSM), Juno – Double Brushed (77% Polyester, 23% Spandex, 230–240 GSM), and Cotton Air (100% Cotton, 210–230 GSM). This category strikes the perfect balance of supportive compression, complete opacity (preventing transparency during deep stretches), and plush layering comfort. It is the premier weight range for form-fitting leggings, supportive sports bras, and cozy athletic hoodies.
- Heavyweight / Structured (250–260 GSM): Represented by our Lola Rib (63% Viscose, 34% Poly, 3% Spandex, 250–260 GSM). Featuring a substantial structural weight and a rich 10×2 rib structure, this fabric delivers high opacity, excellent shape retention, and a luxurious drape. It is specifically designed for statement athleisure wear that transitions seamlessly from fitness studios to high-end streetwear.
Backed by Strict Quality Control (QC) Standards
In the competitive landscape of fashion and apparel production, exceptional quality is never a matter of chance. Behind every flawless seam, perfectly matched color shade, and market-ready clothing collection lies a rigorous, uncompromising system of operational oversight: Quality Control (QC). For emerging fashion startups, indie designers, and established global brands alike, partnering with a garment manufacturing facility in Bali that enforces strict, multi-tiered QC standards is the ultimate differentiator between retail success and costly, reputation-damaging production failures.
What Is Quality Control in Garment Manufacturing?
Quality control (QC) is a comprehensive, systematic inspection and evaluation framework implemented across every phase of the apparel production lifecycle. Rather than acting as a superficial final check before packing, professional quality control serves as an operational safeguard designed to actively detect, correct, and prevent defects from entering the final supply chain.
At Bali Garment Manufacturer, quality control is integrated directly into daily operations, spanning raw fabric intake, sample room prototyping, precision cutting, expert stitching, hardware stress-testing, and final packaging. Every micro-detail—from stitch density and seam allowances to zipper smoothness and label placement—is systematically measured against strict, pre-approved technical specifications.
What Parts of Manufacturing Involve Quality Control?
A truly comprehensive quality control protocol leaves no room for oversight, covering every structural and aesthetic component of garment construction. At our Bali manufacturing facility, quality control is partitioned into specialized inspection checkpoints:
- Stitch Density and Seam Integrity: Inspectors meticulously measure stitch density to ensure it meets the standard of 10 to 12 stitches per inch (SPI) as outlined in the tech pack. Every stitch must be straight, consistent, and entirely free of wandering lines or puckering. Furthermore, overlock and overedge seams are inspected to ensure that the thread interlooping is dense, neat, and fully covers the raw edge of the fabric without cutting into or compromising the material fibers.
- Zero Tolerance for Skipped or Broken Stitches: Initial and final thread locks (such as back-stitches and bar-tacks) must consist of a minimum of 3 to 4 tightly bound steps to prevent unraveling. All alur jahitan (stitching paths) undergo a 100% visual inspection to maintain a strict zero-tolerance standard for skipped stitches or broken threads.
- Trims, Hardware, and Accessory Functionality: All accompanying hardware—including zippers, buttons, elastic bands, drawstrings, snap buttons, and velcro—undergoes rigorous functional stress-testing. Zippers are tested for smooth, snag-free opening and closing over multiple cycles. Elastics are stretched to their maximum thresholds to guarantee reliable recovery without losing elasticity or becoming “dead,” and snap buttons are tested to ensure secure locking without ripping the surrounding fabric.
- Symmetry, Proportions, and Cleanliness: Garment panels are folded and cross-examined to ensure 100% left-to-right symmetry across necklines, shoulder lengths, armholes, and pocket placements. Additionally, finished pieces undergo thorough cleaning checks to ensure absolute freedom from machine oil stains, chalk marks, stray lint, or dust under high-intensity lighting.
Why Do We Need Strict Quality Control?
Implementing an uncompromising, rigorous QC protocol is essential for safeguarding a brand’s financial investment, customer satisfaction, and long-term market reputation. Neglecting quality assurance often leads to severe operational roadblocks:
- Eliminating Costly Production Waste and Returns: Catching structural defects, sizing grading errors, or fabric inconsistencies during the sampling phase or initial batch inspection prevents entire production runs from failing at retail. This proactive approach saves brands thousands of dollars in customer returns, chargebacks, and expensive remanufacturing costs.
- Guaranteeing Absolute Brand Consistency: Modern consumers expect the exact same fit, stretch recovery, color vibrancy, and tactile feel with every purchase. Strict QC ensures that every single garment in a production run strictly matches the approved lab dip, color swatch, and tech pack specifications.
- Protecting Long-Term Brand Credibility: In today’s fast-paced digital marketplace, a single poorly manufactured batch featuring loose threads, jammed zippers, or sheer, non-squat-proof fabrics can result in negative reviews and permanent damage to a brand’s prestige. Flawless physical execution builds unshakeable consumer trust and repeat buyers.
How Do We Ensure Uncompromising Quality Control?
Achieving faultless manufacturing execution requires clear technical benchmarks, trained personnel, and disciplined inspection protocols. At Bali Garment Manufacturer, quality is enforced through strict operational procedures and defined disposition outcomes:
- Advanced Lighting and Material Testing: Fabric rolls are unfurled and inspected across dedicated tables equipped with bright D65 daylight illumination to catch surface flaws, pinholes, pulling, or subtle color shading variances between panels. Color matching is verified directly against approved client lab dips.
- Rigorous Disposition (Disposition) Protocols: Every inspected sample and production garment is evaluated and assigned a definitive status based on strict performance parameters:
- PASS: The sample or garment fulfills 100% of the stringent quality criteria without any flaws.
- PASS WITH COMMENTS: Applied strictly when minor, non-structural cosmetic imperfections (such as an unclipped stray thread end) are discovered, which can be cleaned and corrected immediately within a 5-minute window.
- REJECT / REWORK: Triggered instantaneously if inspectors encounter structural faults, misaligned closures, color mismatches, jammed zippers, or fatal fabric defects. These items are immediately pulled and sent back for comprehensive rework or complete remaking.
Lets Start to Build Your Next Activewear Line with Us
Choosing high-performance technical fabrics combined with strict quality control is the secret weapon to building a loyal, repeat customer base that genuinely trusts your brand. In today’s crowded fitness apparel market, standing out takes more than just a cool design—it takes a bulletproof production process. By partnering with an experienced manufacturing team in Bali, you get hands-on support every step of the way.
You can easily source custom performance blends tailored to your exact needs, touch and test physical fabric swatches to check stretch and hand-feel, and turn your mood boards into retail-ready activewear with zero guesswork. Whether you are scaling an established label or launching your very own startup collection, having expert manufacturing partners ensures your tech packs come to life exactly the way you envisioned.
Ready to bring your next collection to life? Reach out to our manufacturing team today to browse our complete fabric library, request physical swatches, and start your tech pack process with total peace of mind.